
專業CNC加工製造商與出口商
客製化CNC加工零件,安心製造、準時交付
位於中國安徽合肥的3,000 m²製造廠,提供CNC銑削、車削、五軸加工、鈑金與表面處理——每月產能10,000件,通過ISO 9001與IATF 16949認證。報價、生產與全球交貨,單一窗口搞定。
Popular searches: 5-Axis CNC MachiningAluminum CNC MachiningCNC Turning
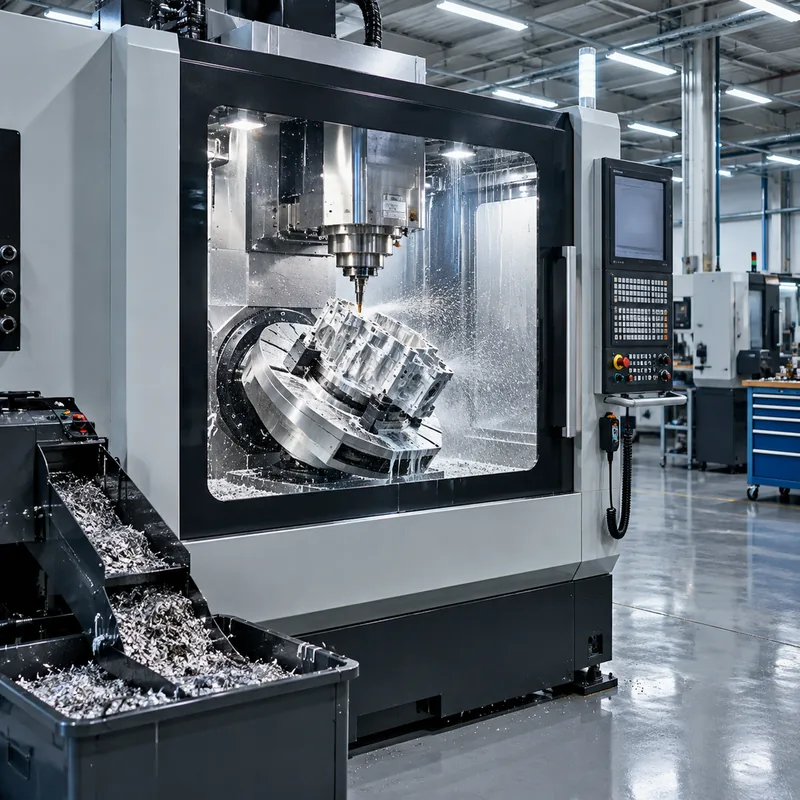
圖片:CNC 加工設施的 AI 生成示意圖。
關於 CNC Machining Hub
CNC Machining Hub 是什麼?
為工程師、產品開發者與採購專業人員提供的工業製造與採購資源。
CNC Machining Hub 提供客製化加工零件的CNC加工資訊、製造能力、材料與製程知識,以及採購資源。技術內容與生產服務來自同一個源頭:我們位於中國安徽合肥的自有製造工廠,創立於2013年,並通過ISO 9001與IATF 16949認證。
本平台使用 Google API(包括 Google Ads API)進行關鍵字與市場研究——以了解搜尋需求並提升技術與商業內容的相關性。Google API 資料僅用於研究與內容規劃。我們不會使用 Google Ads API 資料代表使用者建立或管理廣告活動。
服務項目
CNC加工服務
您只需要提供一張圖面。選定制程、材料與表面處理——我們負責DFM檢討、加工、檢驗與出貨。
CNC加工服務
客製化CNC加工服務:依您的3D圖面,對金屬與塑膠零件進行銑削、車削與五軸加工。從試作品到中小量產,工廠直營。
CNC銑削服務
適用多面體與複雜零件的客製化CNC銑削服務:依您的CAD檔案,對鋁、鋼與塑膠零件進行3–5軸銑削。試作快速,品質穩定。
CNC車削服務
適用軸件、襯套、接頭與圓形零件的客製化CNC車削服務:具動力刀塔的CNC車床加工,依您的圖面從試作到量產。
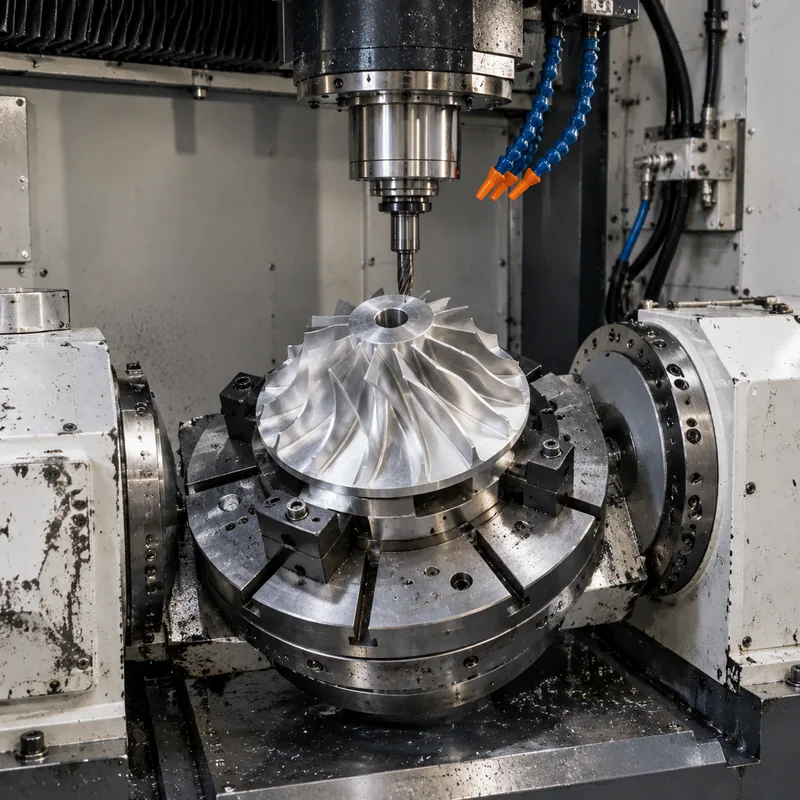
五軸CNC加工服務
五軸CNC加工是一種減材製造製程:切削刀具沿三個直線軸(X、Y、Z)移動,同時工件或主軸繞另外兩軸(通常標示為A與B)旋轉。
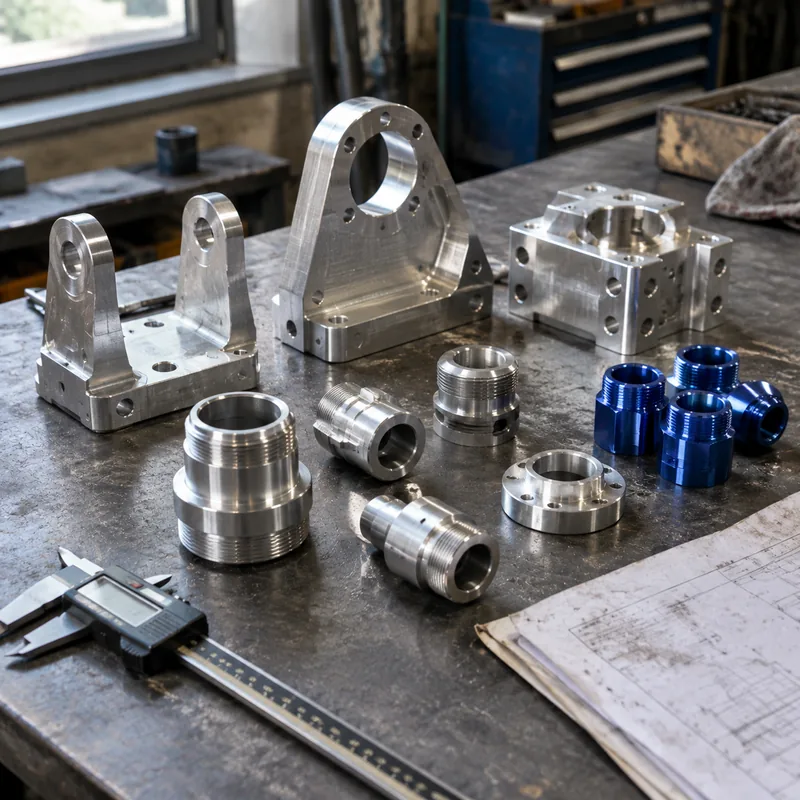
鋁合金CNC加工
鋁合金CNC加工服務:6061與7075零件依圖面銑削與車削,陽極處理提供本色、黑色與客製色。從試作品到量產。
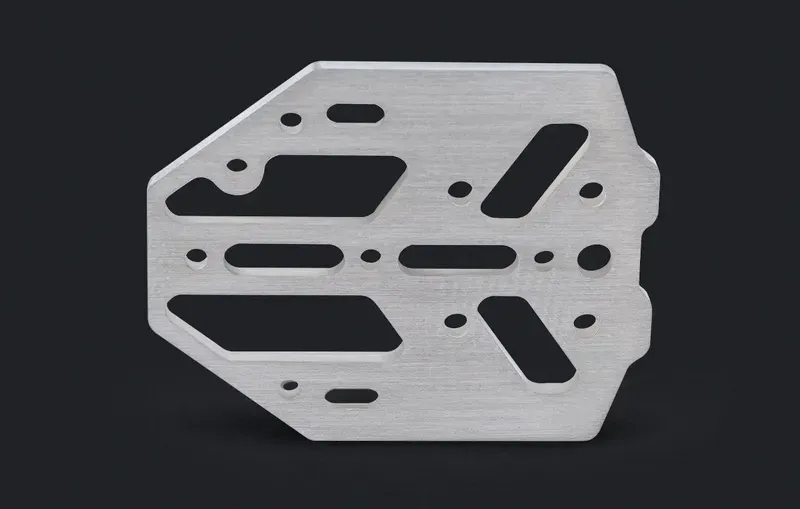
不鏽鋼CNC加工
不鏽鋼CNC加工服務:303、304與316零件依圖面車削與銑削,搭配鈍化處理與電解拋光。食品、船舶與工業級皆可。
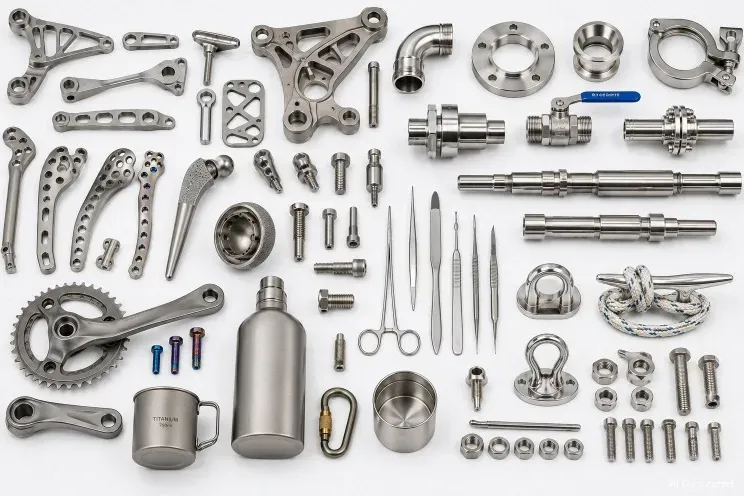
鈦合金CNC加工
鈦合金CNC加工服務:Ti-6Al-4V 與工業純鈦牌號依圖面加工,適用輕量化、耐腐蝕與生物相容性零組件。
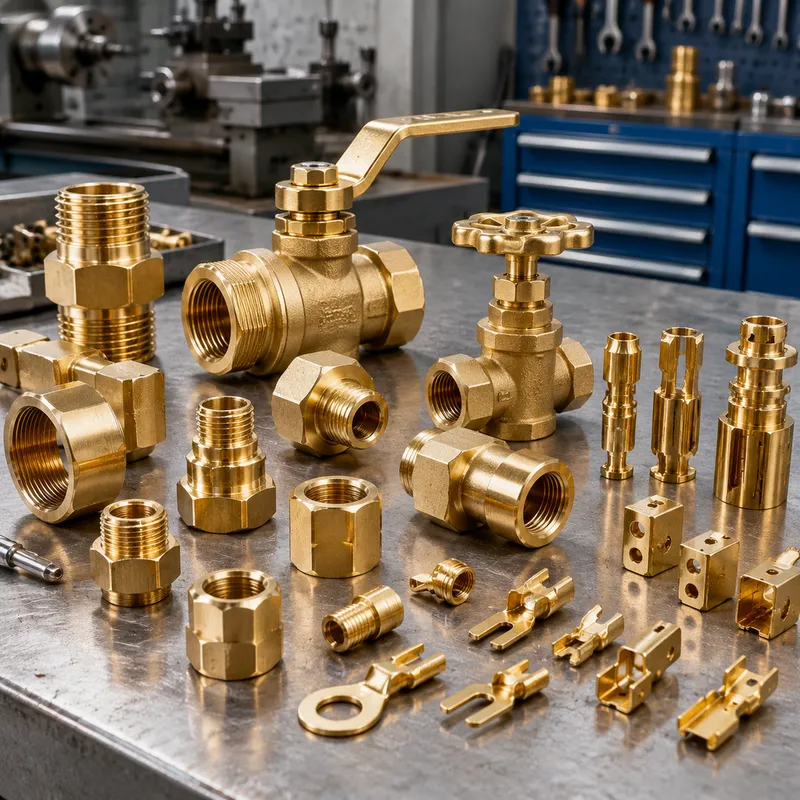
黃銅CNC加工
黃銅CNC加工服務:C36000 易切削黃銅與 C260 彈殼黃銅零件依圖面銑削與車削,可搭配鉻酸鹽皮膜、鍍鎳與鍍錫。接頭、閥件與電氣零組件。
加工能力
核心加工能力
採購人員下圖前必看的數據——可達公差、標準交期與最小訂購量。
- ±0.1–0.2 mm 標準
- ±0.05 mm or tighter 精密
- 15–25 天 標準交期
- 1 件起 試作品MOQ——無強制最低量
產業應用
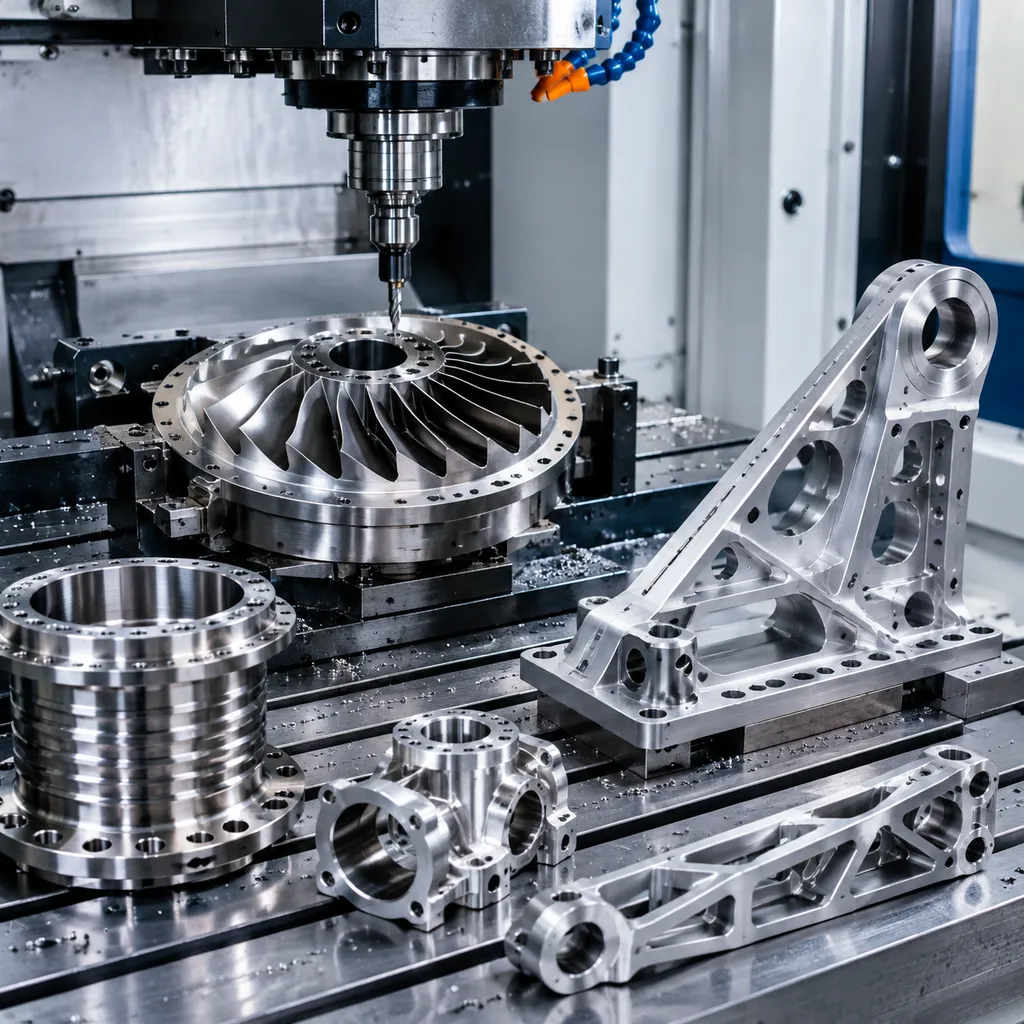
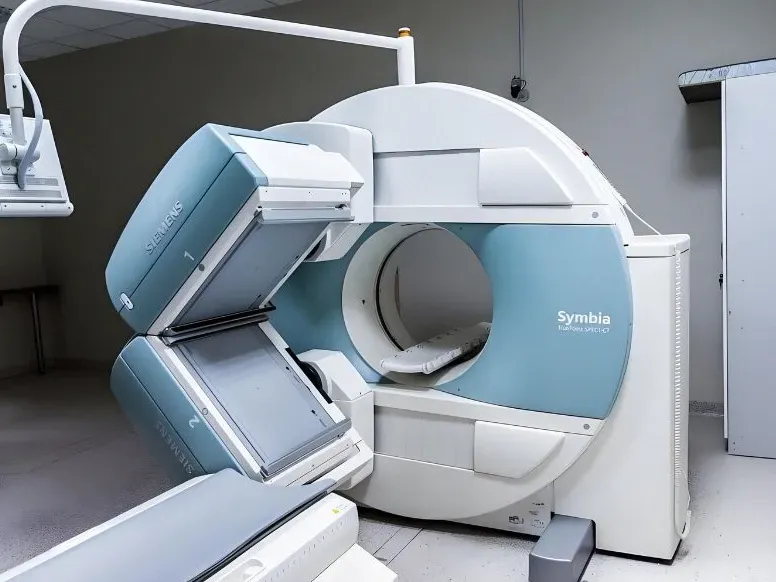
依產業分類的CNC加工
為高要求產業提供客製化零件——依您的圖面加工,每批皆經檢驗。
材料
我們加工的材料
常備工程金屬與塑膠材料,交期快速。特殊合金可依需求洽詢。
- 鋁合金 6061/7075
- 不鏽鋼 303/304/316
- 碳鋼與合金鋼
- 黃銅與銅
- 鈦合金 Ti-6Al-4V
- PEEK / Delrin / 尼龍
選擇我們的理由
買家為何選擇 CNC Machining Hub
從報價到交貨的單一負責窗口——來自我們合肥自有工廠的精密製造,品質管制內建於每個環節。
單一夥伴,涵蓋所有CNC製程
CNC銑削、車削、五軸加工、鈑金與表面處理——依您的零件幾何、數量與公差,在合適的設備上廠內生產。
從試作到量產
下訂單一件試作品或擴充到數千件皆可。沒有最小訂購量,從首件到量產品質始終一致。
工廠直營價格
我們在合肥自有產地製造,每月產能10,000件——價格具競爭力,無貿易商加價。
可驗證的品質
通過ISO 9001與IATF 16949品質管理系統認證,製程中檢驗與出貨前終檢報告可依需求提供——零件出貨前完成尺寸確認。
中國採購
為什麼買家選擇從中國採購CNC零件
成熟的CNC供應體系、具競爭力的工廠直營價格,加上英語工程支援,讓中國成為客製化加工零件的首選採購地。我們結合在地工廠產能與出口級品質管制,讓海外買家同時取得價格與交付的可靠性。
- ✓工廠直營價格,無貿易商加價
- ✓生產前對每張圖面提供DFM檢討
- ✓每批出貨附尺寸檢驗報告
- ✓出口包裝與全球運輸經驗
作業流程
從您的圖面到交付零件
五步驟的製造流程,每個階段都內建品質管制。
- 提交詢價 — 寄送3D檔案(STEP、STP、IGS)與2D圖面,並附上數量、材料與表面處理需求。
- 收到附DFM檢討的報價 — 我們評估可製造性,在相關之處建議節省成本的改善方案,並回覆明確報價。
- 確認後即排定生產 — 您的專案依零件幾何、數量與公差安排至合適的設備進入生產。
- 製程中品質檢驗的生產 — 零件在我們的品質管制下加工,並在約定的檢查點執行首件與製程中檢驗。
- 終檢與全球交貨 — 可依需求提供尺寸報告與材料證明,隨後以可追蹤貨運送達您的門口。
知識庫
探索CNC加工
以工程為本的指南,說明零件如何被製造出來——各製程能達到什麼、成本由什麼驅動、以及在哪裡會出問題。內容提煉自多來源產業研究語料庫。
When 201 Stainless Sheet Can Replace 304: Corrosion, Forming and Welding Limits
201 is the lower-corrosion-resistance, lower-cost option relative to 304, consistent with its lower chromium and roughly half the nickel content, and it is positioned for short-term, decorative or cost-sensitive uses where extreme corrosion resistance is not required. 304 is positioned for long-term outdoor and food-grade service, and even 304 is limited against chlorides, so chloride-rich or marine service is a condition where neither grade is the highest-resistance choice. No source in this set quantifies corrosion rates, chloride thresholds or service-life differences for 201 versus 304 in a defined environment, so the accept/reject line for a specific service environment remains unresolved and must be set by the buyer's own test or supplier data.
Read article →304 vs 316 Stainless Sheet for Corrosive Service: When the Upgrade Is Indicated and What the Premium Costs
For marine, chemical or persistently chloride-bearing service, the available sources consistently direct buyers to 316/316L, while 304 is presented as adequate for moderate, indoor-dry or general atmospheric exposure. Budget the upgrade at roughly a 20–40% material price premium over 304, to be confirmed by quotation at your thickness and finish. No source sets a numeric chloride or temperature boundary, so the grade call stays a judgement you must document.
Read article →5-Axis vs 3-Axis vs EDM for Complex Dies: Which Geometry Justifies the Premium
For a complex die, 5-axis is justified when undercuts, compound angles or freeform surfaces force more than one or two tool orientations, because single-setup machining removes re-fixturing error and can cut benching on curved and deep features. Where every feature is reachable from one or two orientations, or by indexed 3+2 positioning, the higher machine rate and CAM cost of 5-axis buy nothing. EDM stays relevant for conductive hard material, but it removes material slowly, needs electrode fabrication and leaves a recast layer that usually requires post-finishing.
Read article →5-Axis CNC vs 3-Axis vs EDM for Complex Molds: Where the Evidence Supports the Choice
For a complex mold with curved surfaces and features on several faces, 5-axis machining cuts setups, re-clamping error and hand polishing relative to 3-axis. But it carries a higher machine rate and longer CAM programming time. The premium is only defensible where complexity would otherwise force multiple 3-axis setups or heavy benchwork; for simple prismatic cavities 3-axis is likely faster and cheaper. EDM is a conductive-material process with slow removal and electrode wear, and the sources give no matched finish, lead-time or cost comparison against 5-axis for a specific cavity.
Read article →5052-H32 vs 6061-T6 for a Bent and Welded Sheet Metal Enclosure: When the Strength Upgrade Is Worth the Forming and Welding Penalty
For a bent and welded enclosure, 5052-H32 is the more suitable alloy when tight-radius bending and welding without post-weld heat treatment are priorities, because it forms to tighter radii and retains more heat-affected-zone strength. 6061-T6 is justified only when the enclosure genuinely needs its higher yield strength and the bends can be kept generous or formed in a softer temper before heat treatment. The sources do not fix a minimum bend radius for 6061-T6, a per-pound cost difference, or a lead-time comparison, so those must be verified with the fabricator.
Read article →