
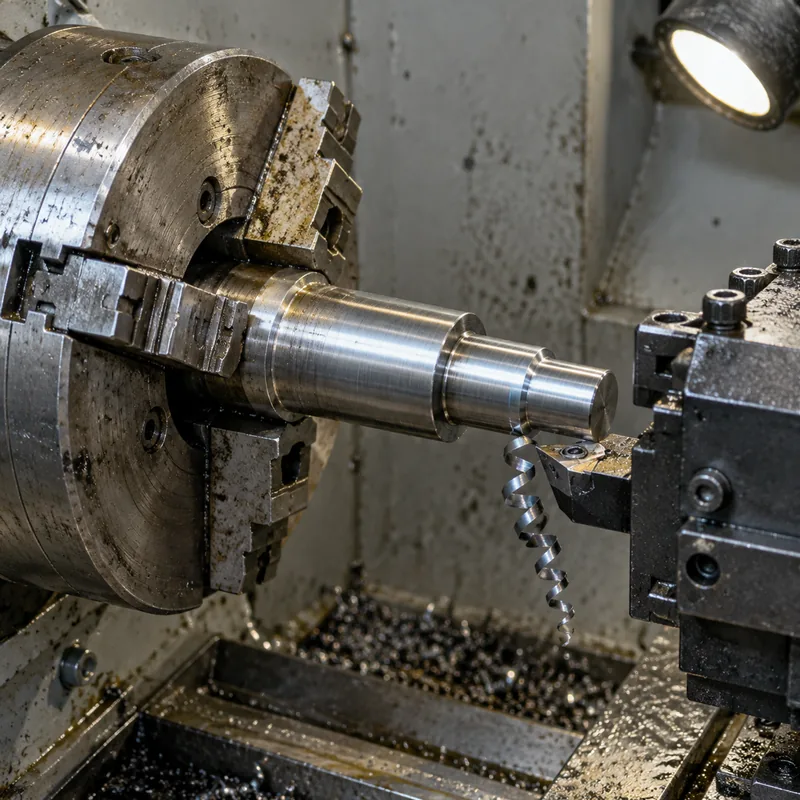
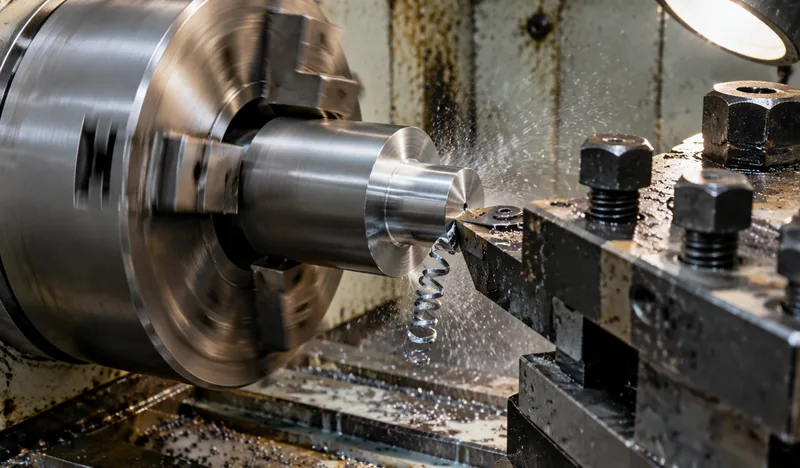
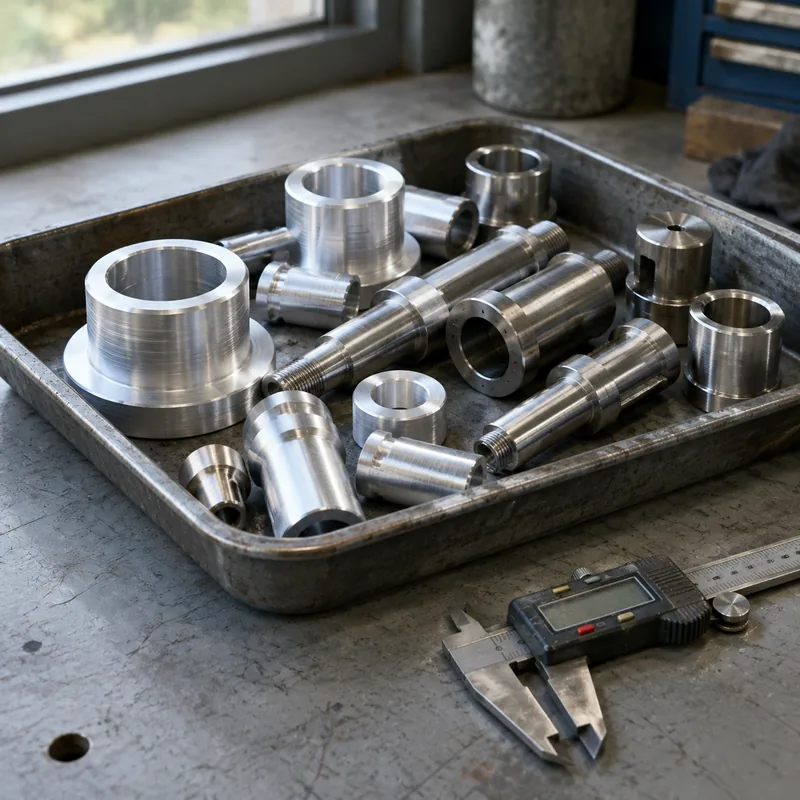
Our CNC turning services produce shafts, bushings, spacers, fittings and other rotationally symmetric parts on CNC lathes with live tooling, so milled flats, cross holes and threads are done in one setup.
Bar-fed work keeps per-piece cost low for volume runs, while chuck work handles flanged and irregular blanks for prototypes and low volumes.
Capabilities
- CNC turning diameters from 2 mm to 350 mm
- Live-tooling for cross features in one setup
- Thread turning and thread milling
- Bar-fed volume production
Typical materials
Stainless steel 303/304/316, carbon steel, aluminum, brass 360, copper, titanium, plastics.
| Material / grade | Typical condition | Machinability | Where it fits |
|---|---|---|---|
| Aluminium 6061 | T6 (solution treated and aged) | Easy: free-cutting, good chip control | Brackets, housings, fixtures, prototypes into production |
| Aluminium 7075 | T6 / T651 | Harder: more tool wear, needs rigid setups | High-strength, weight-critical parts; not for welding |
| Stainless 304 / 304L | Annealed | Work-hardens: slower speeds, positive feed | General corrosion resistance, food and process equipment |
| Stainless 316 / 316L | Annealed | Tougher than 304: more tool wear | Chloride, marine, medical and pharmaceutical exposure |
| Carbon steel 1018 / 1045 | As-rolled / normalised | Easy to moderate; needs protection against rust | Shafts, plates, weldments, tooling bodies |
| Brass C360 | H02 half hard | Excellent: high speeds, clean finish | Fittings, bushings, connectors, decorative parts |
| Copper C110 | Annealed / H02 | Gummy: sharp tools and high rake angles | Conductivity, busbars, thermal management |
| Titanium Grade 5 (Ti-6Al-4V) | Mill annealed | Difficult: low speeds, heat control, tool wear | Aerospace, medical and lightweight high-strength parts |
| Engineering plastics (POM, PEEK, PA) | Extruded / annealed | Easy to gummy: soft jaws, sharp tooling | Insulation, low friction, chemical and wear parts |
Finishes
As-turned, polishing, passivation, nickel plating, black oxide, anodizing (aluminum).
| Finish | What it does | Specify it when |
|---|---|---|
| As machined | Tool marks left visible; Ra typically 1.6-3.2 µm | The part only has to function |
| Bead blast | Uniform matte surface, hides tool marks | Cosmetic parts before anodising |
| Anodising Type II | Builds an oxide layer; colour options | Aluminium appearance plus mild corrosion and wear resistance |
| Hard anodising Type III | Thicker, harder oxide layer | Sliding or wearing aluminium surfaces |
| Chromate conversion | Thin protective film that stays conductive | Electrical bonding or grounding on aluminium |
| Electroless nickel | Uniform, hard, corrosion-resistant layer | Wear plus corrosion, including inside bores |
| Zinc plating | Economical sacrificial corrosion protection | Steel parts in indoor or sheltered service |
| Powder coat | Thick, durable, decorative layer | Appearance is the requirement |
| Passivation | Removes free iron and restores the oxide film | Stainless parts after machining |
| Stress relief / heat treatment | Relieves residual stress before or after cutting | Thin walls and tight tolerances that must survive machining |
Tolerances
Diameter tolerances to ±0.01 mm; tighter on request after drawing review.
| Callout | What it needs | Effect on cost and lead time |
|---|---|---|
| General: ±0.25 mm / ±0.010 in | Standard tooling, dimensional check | Baseline: no adder |
| Standard: ±0.13 mm / ±0.005 in | Machine in good condition, first-article check | Small adder; the usual quoting default |
| Tight: ±0.025 mm / ±0.001 in | Ground or diamond tooling, temperature control, CMM | Step change: slower cuts plus full inspection |
| Precision: ±0.013 mm / ±0.0005 in | Finish passes, gauging, controlled environment | Machining dominates the price; often a separate operation |
| Position / angularity (GD&T) | Datum control, one setup where features are related | Depends on how many setups the datum spans |
| Surface finish Ra 0.8 µm or finer | Finer stepovers, polishing or a finishing pass | Adds a process step, not just machining time |
Process Options
- Finishing Options: Black Oxide, Electropolishing, ENP, Media Blasting, Nickel Plating, Passivation, Powder Coating, Tumble Polishing, Zinc Plating, Vibratory Tumbling
- EPX 82 is processed using Carbon DLS
- MUD is a type of mold that uses a standard injection molding frame.
- Different taper turning methods suit different jobs. Compound slides often handle short tapers, while CNC interpolation and taper attachments improve repeatability on longer parts
- G92 is used by programming one or more G92's right after the G76 threading cycle
- Estimates are provided through an auto-quoted method.
- EDM relies on a voltage and a thin wire
- Electropolishing is an electrochemical process.
- Water jet cutting is used for cutting sheet metal.
Surface Finish Reference
- SPI A-1 has a surface roughness of 0.012–0.025 µm.
- SPI B-2 has a finish of Medium semi-gloss.
- SPI B-2 has a surface roughness of 0.10–0.15 µm.
- SPI C-3 has a surface roughness of 0.63–0.70 µm.
- Super high gloss, polished with a Grade #3 (6000-grit) diamond buff to Ra 0.012–0.025 µm.
- Medium semi-gloss, finished with 400-grit paper to Ra 0.10–0.15 µm.
- Normal matte, polished with 320-grit stone to Ra 0.63–0.70 µm.
- Very Smooth finish (N5) corresponds to a surface roughness Ra of 0.4 μm.
- A Ra 0.4 µm finish requirement is achievable with a bore diameter tolerance of ±0.0005 inch.
- A sealing surface may need a smoother finish like Ra 0.4.
- Electropolishing achieves Ra <0.4 µm.
- Ra ≤ 0.4 µm is a tighter surface roughness requirement than Ra ≤ 0.8 µm.
- Ra 3.2 µm (125 µin) is a standard machined finish.
- Ra 3.2 micrometers corresponds to 125 microinches Ra.
- Typical as-machined CNC milling surface roughness is Ra 1.6–3.2 µm.
- 1.6 µm Ra surface roughness is achieved by CNC milling and turning in stainless steel.
- 0.4 µm Ra surface roughness is achieved by CNC turning plus polishing in steel.
- Traditional CNC turning is no longer viable when tight surface finish requirements like Ra 0.4 µm are added.
Tolerance Reference
- The tolerance with drawing for CNC Milling is as low as +/- 0.005 mm.
- FDM 3D printing offers a low-cost component with average accuracy and uses thermoplastics for 3D printing.
- Wire Cut EDM is highly accurate.
- Die sinker EDM is capable of maintaining tight tolerances
- The shop needs to have CNC machines that can achieve a specific tolerance.
- Angularity tolerance defines a zone
Industries We Serve
- antennas
- automotive
- CNC machined parts
- considered
- custom parts
- electronics
- medical diagnostic
- optical displays
Material Reference
- ABS
- Carbon steel
- ceramic
- composites
- epoxy resin
- Hardened Materials
- High Impact Polystyrene
- Low-density polyethylene
- MDF
- metal
- Plastic
- Polybutylene Terephthalate
- SUS304
- thermoplastics
- thick metal sheets
- tungsten carbide
Ordering, Lead Times & MOQ
Custom CNC parts carry no forced MOQ; ordering from a single prototype piece is standard industry practice.
Instant-quote platforms publicly advertise prototype lead times of 1-3 business days.
Online RFQ is the industry-standard flow: upload a 3D model (STEP/STP/DWG/DXF), receive an instant quote or engineer review, then production, inspection, and delivery.
Frequently asked questions
Can you do Swiss-type turning?
Small, long and slender parts are turned on Swiss-type lathes to our inspection standard; tell us the part and we will confirm the process route.
What quantities make sense for turned parts?
Prototypes from 1 piece are welcome. Bar-fed production becomes cost-effective from a few hundred pieces depending on the part.
Do you handle surface finish callouts like Ra values?
Yes. Specify Ra on the drawing and we process accordingly, with surface measurement on request.
What is the minimum order quantity (MOQ)?
Prototypes from 1 pc. Low-volume production typical 50-500 pcs. No forced MOQ on custom parts; unit price drops with volume.
What is the typical lead time?
Industry benchmark: instant-quote platforms deliver prototypes in 1-3 business days. Our own production: prototypes 5-10 working days, including in-house QC and shipping. Production: 2-4 weeks depending on quantity/finishing. Express options exist; finishing adds days.
How do I get a quote and what information do you need?
3D files (STEP/IGS) + 2D drawing with tolerances. Material, quantity, finish, destination country. Quote turnaround: 24-48h typical.
What tolerance should I specify?
Specify tight tolerances only on critical features. Standard ±0.1 mm covers most features. Tighter tolerance = cost multiplier; apply selectively via drawing GD&T.
How is quality controlled?
First-article inspection in our own shop before the first production order. In-process checks. Final inspection report (dimensions) with shipment. Material certs (mill test reports) on request.
Is my design protected?
NDA before file exchange. Files used only for your production. No resale of custom designs.
Which material should I choose?
Function first: strength, weight, corrosion, cost. Common pairings: 6061 general, 304/316 corrosive env., PEEK medical. See materials guide pages.
How do you ship and what terms?
DHL/FedEx/UPS express for samples and small batches. Air/sea freight for production volumes. Incoterms: EXW/FOB/DAP/DDP options.
Sources · 1
- hubs.comIndustry peer technical page
Technical references cited for verifiability — not supplier recommendations.Browse the research library.